ABOUT US
Beijing Antaios Technology Co., Ltd. specializes in engine power solutions for small and medium‑sized construction machinery. With 10 years of expertise, we provide customized solutions and strict factory bench testing with complete test reports and traceable data to ensure reliable quality.
GET A FREE QUOTE

What Should You Test After Installing a Deutz F4L912 Replacement Engine?
-
 author
- 24,September
 author

The engine starts cleanly and holds idle. Then the machine begins working: a hydraulic function slows, engine speed dips, or temperature keeps climbing as the compartment warms up. A successful first start has not answered the question that matters most: can the replacement engine do the machine’s job throughout its normal working cycle?
After installing a Deutz F4L912 replacement engine, validate load response, cooling-air performance, lubrication, controls and the machine’s actual output. Compare recorded results with the operating limits agreed for that exact engine and equipment configuration. A factory bench-test report is valuable, but it does not replace testing with the machine’s enclosure, drive system and working load.
For construction equipment, begin with the bare-engine installation and the systems connected to it. Acceptance depends on how those systems work together, not simply on whether the engine mounting points line up.
What Does Machine Validation Add to a Bench Test?
Machine validation is the controlled evaluation of an installed engine while the equipment performs its intended work. It checks whether engine response, temperatures, controls and machine output remain within the agreed operating limits under recorded conditions. The result applies to the tested configuration and duty, not every possible application.
An engine dynamometer and a construction machine place different demands on the installation. The machine adds its own air path, exhaust routing, hydraulic or mechanical drive, control linkage and changing load. Those differences explain why both levels of testing matter.
| Test level | Main question | Useful evidence |
| Engine bench test | Does the configured engine meet its agreed test points? | Engine identity, test conditions and measured results |
| Initial machine run | Do the connected systems operate correctly? | Starting, instruments, controls and inspection record |
| Working-cycle validation | Can the installed combination perform the required task? | Load response, temperature trends and machine-output record |
ANTAIOS POWER’s engine bench-testing process provides engine-level evidence. Keep that report with the machine test record so any difference can be investigated against a known configuration.
Define Acceptance Before Applying Load
The F4L912 is a four-cylinder, naturally aspirated, air-cooled platform. That is useful identification, but it is not a complete acceptance specification. Within a Deutz 912 engine replacement project, the selected power rating, operating speed, governing arrangement and accessories must match the particular machine.
Record the replacement engine’s serial number, configuration and rated operating point before testing. Add the machine model, driven equipment, installation drawing revision and intended working cycle. If a coupling, cooling-air duct or control component has changed, include the change in the record.
The test plan also needs an agreed target for the machine itself. For a hydraulic machine, that may include a defined function and cycle time at a specified load. An acceptable engine-speed reading alone does not show that the hydraulic system delivers the required output.
Decide which instruments will measure engine speed, oil pressure and temperature, and which machine-side measurements are needed. Establish permissible limits, test duration and stop conditions from the exact engine and equipment instructions. There is no single temperature limit or speed-drop percentage that approves every F4L912 installation.
Qualified commissioning personnel should run the tests in a controlled area with ventilation, guards and the machine’s safety measures in place. Stop under the applicable emergency procedure for loss of oil pressure, fuel leakage, uncontrolled speed, severe vibration or overheating. Do not bypass protective devices to complete a test.
Check the Deutz F4L912 Through Its Working Cycle
Start with low-demand operation and progress through the approved load stages. Keep the test conditions comparable between runs. A result recorded with different engine speed, ambient conditions or machine settings may not explain whether a modification helped.
Establish Starting and Warm-Up Behavior
Confirm that the starting system operates correctly and the engine settles into stable running. Check the installed instruments and warning indications against the commissioning instructions. Record oil pressure and the relevant temperature readings as the engine warms up, rather than noting only that it started.
Inspect for leakage and abnormal noise using safe inspection methods. Observe the throttle or speed-control response before asking the machine to perform demanding work. A control that sticks, responds inconsistently or fails to return as intended needs investigation before the load is increased.
Measure Response When the Machine Takes Load
Apply the representative working load through the machine’s approved test procedure. Record the selected engine speed, the lowest speed reached as load changes, and how the engine settles after the change. Repeat the same task to see whether the response is consistent.
For hydraulic equipment, record the corresponding machine function as well. If the task slows while engine speed remains steady, the investigation should include the hydraulic controls and drive system. If speed falls sharply as the task begins, review both engine response and the load demanded by the machine. Either observation is a starting point for diagnosis, not proof that one component is at fault.
Do not increase hydraulic pressure settings or override load controls to force an acceptance result. The engine and driven system must stay within their approved operating limits.
Evaluate Cooling With the Enclosure in Its Working Position
A Deutz F4L912 replacement engine relies on cooling airflow through the engine’s cooling arrangement. Inspect the blower drive, air passages, shrouding and cooling surfaces against the installed configuration. Combustion intake air and cooling air serve different purposes; a clear air filter does not demonstrate adequate engine cooling.
Run the thermal assessment with access panels and guards in their normal operating positions. An open engine compartment can change airflow and conceal a problem that returns after the machine is closed for work. Record ambient conditions, engine load and temperature trends together.
The question is whether temperatures stabilize within the agreed limits during the required duty. A rising trend near the end of a short run is not the same as a stable result. The responsible engineer should define sufficient test duration for that installation and operating condition.

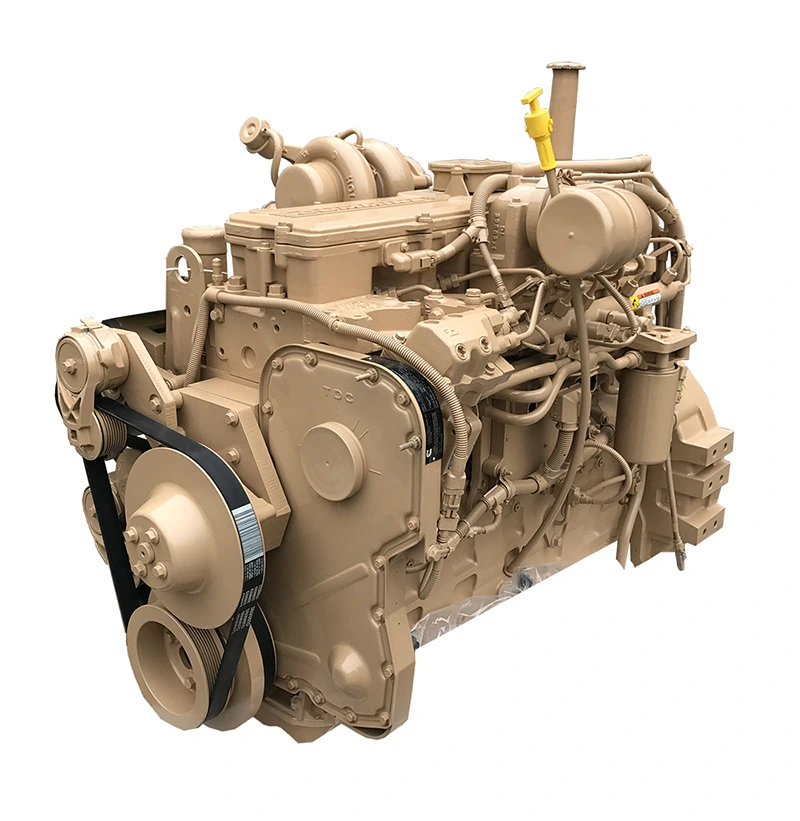
The 912-series engine shown illustrates the blower and shrouding arrangement. Engine appearance and accessory layout vary with the selected model and configuration.
Track Lubrication and Check the Connected Systems
Compare oil-pressure readings at the operating points specified for the engine, including the relevant warm condition. Record engine speed and temperature alongside pressure so the result has context. Investigate unexpected readings with suitable test equipment before treating an instrument indication as a confirmed engine fault.
Also inspect the fuel system, exhaust connections, mounts and driven interface after the approved run and shutdown procedure. Look for leakage, abnormal movement, rubbing or heat damage. Isolate the equipment before physical inspection; the applicable instructions determine whether cooling or pressure release is required first.
Verify Controls and Repeat the Normal Task
Check normal stopping and the installed warning or shutdown functions using the approved functional-test method. Do not deliberately starve the engine of oil or block cooling airflow to trigger a protection device. Where an alarm or shutdown function is specified, verify the complete signal path, not just the presence of a sensor.
Repeat the representative operating cycle with the same settings and record the machine output. Include a warm restart when required by the commissioning plan. If engine operation is stable but the machine still misses its task target, acceptance remains unresolved until the cause is understood.
Keep a Test Record That Supports a Decision
A video of the machine running can help explain an event, but it rarely captures all the information needed for acceptance. Pair it with a short record of the operating point, measurements and observations. Time references help engineers connect a speed change with a control input or machine movement.
| Record group | What to include |
| Identification | Engine serial number, configuration and machine model |
| Conditions | Ambient conditions, engine speed, load and enclosure position |
| Measurements | Oil pressure, relevant temperatures and machine-output measurements |
| Observations | Alarms, noise, leakage, speed response and repeatability |
| Decision | Pass, hold for investigation, or retest after a documented change |
“Pass” should mean the agreed criteria were met under the recorded conditions. If a required measurement is missing, keep the result open instead of treating an uneventful run as complete approval. A successful workshop run also does not establish performance at an untested altitude, ambient temperature or duty.
When a change is needed, record what changed and repeat the affected checks. Changing several components at once can make it difficult to identify which change resolved the problem. ANTAIOS POWER’s application-specific technical matching can use engine and equipment operating information to support configuration review.
Conclusion
A Deutz F4L912 replacement engine is ready for machine acceptance when the installed combination meets its agreed working requirements, not merely when it starts. The decisive evidence is repeatable machine output, acceptable load response, controlled temperatures, correct lubrication and functioning controls under the defined test conditions.
Prepare the engine identity, installation details, bench report and machine test record together. To review a replacement configuration or an unresolved validation result, contact ANTAIOS POWER with those records and the equipment’s required operating point.
Frequently Asked Questions
Is a Bench-Test Report Enough to Accept the Installed Engine?
No. A bench report documents engine performance under its stated test conditions. Machine acceptance also requires checking the actual installation, cooling-air path, controls and working load. Use the bench report as a reference, then verify that the complete machine achieves its agreed output within the applicable operating limits.
Which Temperatures Matter on an Air-Cooled Replacement Engine?
Use the engine-temperature and oil-temperature measurements specified for the exact assembly, together with ambient conditions and load. The F4L912 is air cooled, so a generic water-cooled-engine checklist is unsuitable. Any separate machine hydraulic-oil cooling system has its own requirements and does not replace verification of engine cooling.
How Long Should the Machine Validation Test Last?
The duration depends on the approved working cycle, thermal behavior and equipment requirements. It must be long enough to evaluate the agreed operating points and temperature trends safely. A fixed number of minutes cannot approve every installation. Define the duration and stop conditions before testing, using the engine and equipment instructions.
What Should You Send When the Engine Passes but the Machine Does Not?
Send the engine serial number, confirmed configuration, bench report and machine model, plus the load conditions and recorded symptoms. Include synchronized engine-speed readings, relevant temperatures and machine-output measurements where available. Photos of the air path and driven interface can help the technical team determine which part of the installation needs further investigation.
Recent Post



Related Products
Best-selling Products

912/W Series
The 912 series engine is an air-cooled diesel engine with a power range of 14-76 kW and a speed range of 1500-2500 rpm. This series of engines offers a variety of 2, 3, 4, and 6-cylinder options.
The 912W series is an upgraded version of the 912 series. To better suit the underground mining working environment, the 912W series features improved engine emissions.
Over the past decade, ANTAIOS' 912 series diesel engines have been exported to more than 100 countries. This product is mainly used in construction machinery, industrial and agricultural fields.

914 Series
The 914 series diesel engine is commonly used in underground mining environments. This air-cooled engine has a power range of 41-141 kW and a speed range of 1500-2500 rpm. It is available in both naturally aspirated and turbocharged versions to meet your different needs.
Unlike most 914 series engines produced in Chinese factories, ANTAIOS provides genuine German parts for its 914 series engines. This ensures engine quality while offering you a lower price than European brands.

2012 Series
The 2012 series engines are water-cooled engines manufactured by DEUTZ of Germany. This engine series is widely used in the fields of construction and generation. Available in both 4-cylinder and 6-cylinder configurations, common models include the BF4M2012, BF4M2012C, and BF6M2012C. If your equipment is powered by a DEUTZ 2012 series engine, ANTAIOS can provide you with suitable replacement solutions.
Our 2012 series diesel engines cover a power range of 75–155 kW, with speeds reaching 1500–2500 rpm. If you have customized requirements, we can also provide optional configurations, such as the cooling system, tailored to your specific needs

TCD2012/2013 Series
The TCD2012/2013 series is a high-pressure common rail, water-cooled diesel engine. Compared with the standard versions, this engine offers higher emission standards, making it more suitable for applications with stricter emission requirements. In past equipment applications, it has been widely used in underground mining operations.
The TCD2012/2013 series engines supplied by ANTAIOS typically have a delivery time of about one month. If the configuration requirements are relatively simple, the delivery time can sometimes be shortened to around 10 days. Since the TCD2012 series engines provided by ANTAIOS are custom-built, they are not kept in stock. All engines are scheduled for production after your order is placed.

1015 Series
The DEUTZ 1015 series engine is a large water-cooled engine, available in both 6-cylinder and 8-cylinder configurations. Unlike DEUTZ’s other 4-cylinder or 6-cylinder water-cooled engines, this engine features a V-type cylinder arrangement, significantly reducing the space required for installation.
The BFM1015 engines supplied by ANTAIOS are produced by reputable manufacturers in China. These engines are typically used in specialized equipment, where performance requirements are more demanding. Before delivery, each engine undergoes bench testing in accordance with original factory standards, along with additional testing based on specific requirements, to ensure that the engine we provide fully meets your application needs.

TCD2015 Series
The TCD2015 series engine is a V-type, 4-stroke, water-cooled diesel engine. This engine is available in V6 and V8 models, with power outputs ranging from 240-500 kW and a common operating speed of 2100 rpm. It meets Euro III emission standards and above. This engine is widely used in construction machinery, generator sets, mining equipment, marine power, and oil and gas equipment.
In addition to customizable configurations, ANTAIOS also offers custom paint colors. Unless otherwise specified, we generally offer gray paint.